
PVD hard coatings: ceramic on the bearing surface
Titanium nitride, titanium niobium nitride, zirconium nitride and DLC make joint surfaces and instruments harder and more wear-resistant. They keep nickel, cobalt and chromium in the base material. Produced in a dedicated building in Rostock since 2019.
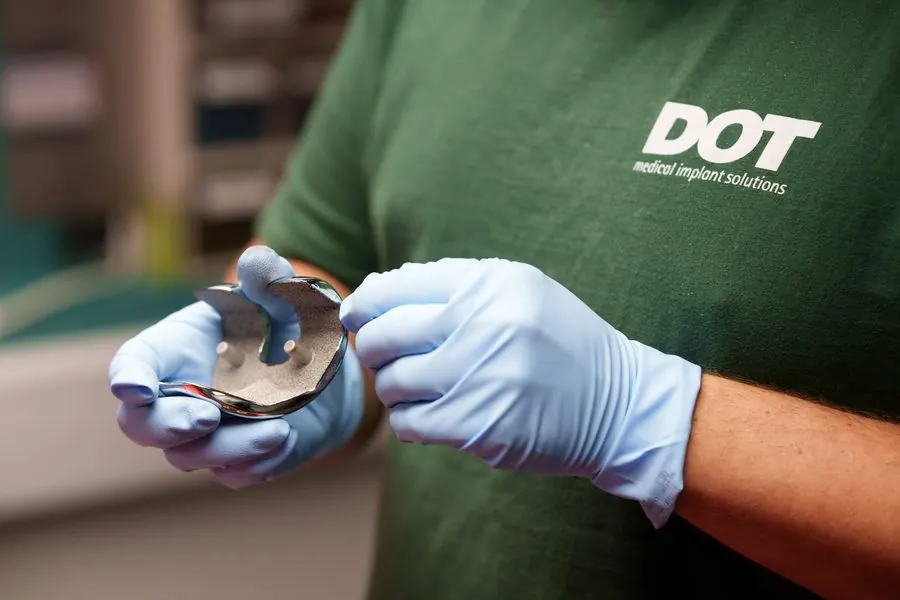
With every step, a knee joint slides against itself.
This causes wear, and tiny amounts of nickel, cobalt and chromium can pass from the metal into the tissue.
- Thin. The ceramic layer is a few thousandths of a millimetre thick.
- Hard. It slides more easily and wears less than the metal beneath it.
- Dense. It keeps the metal ions where they belong: in the component.
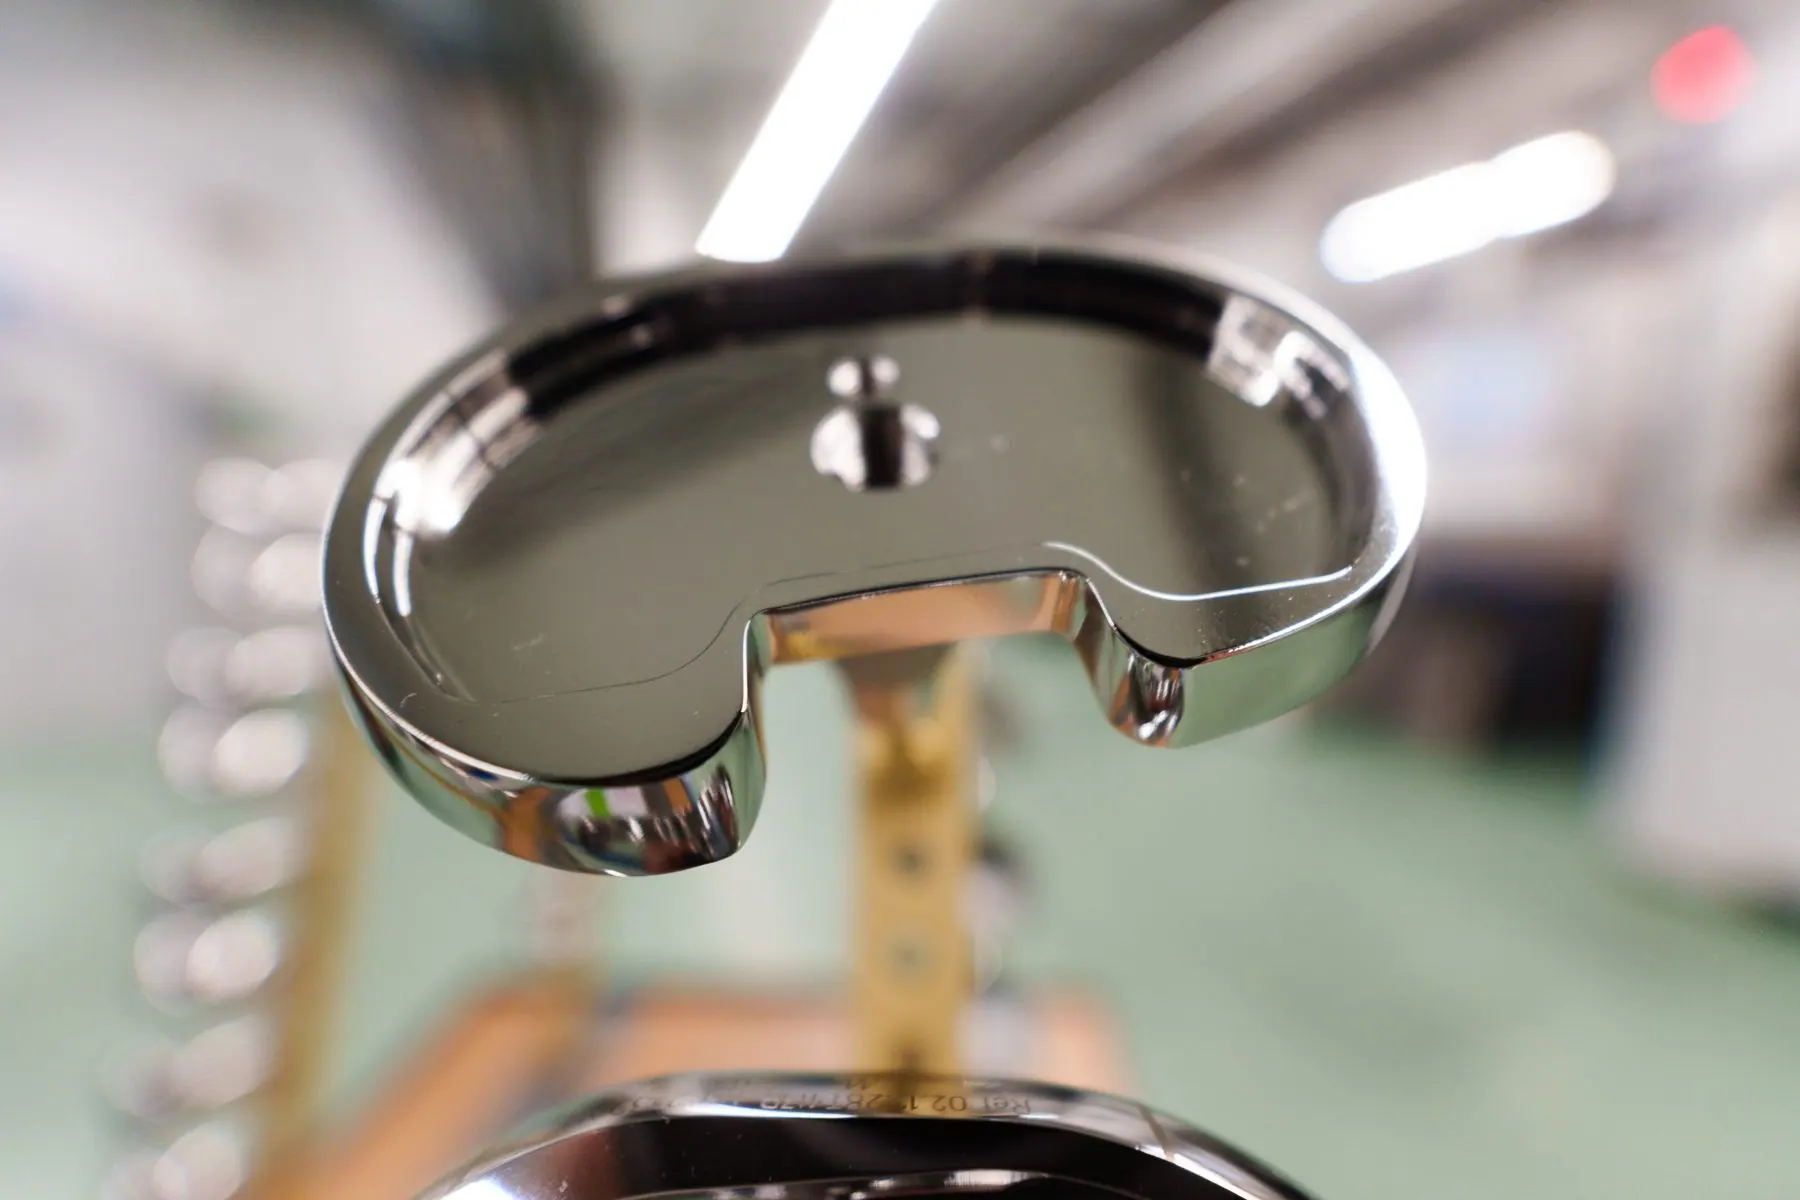
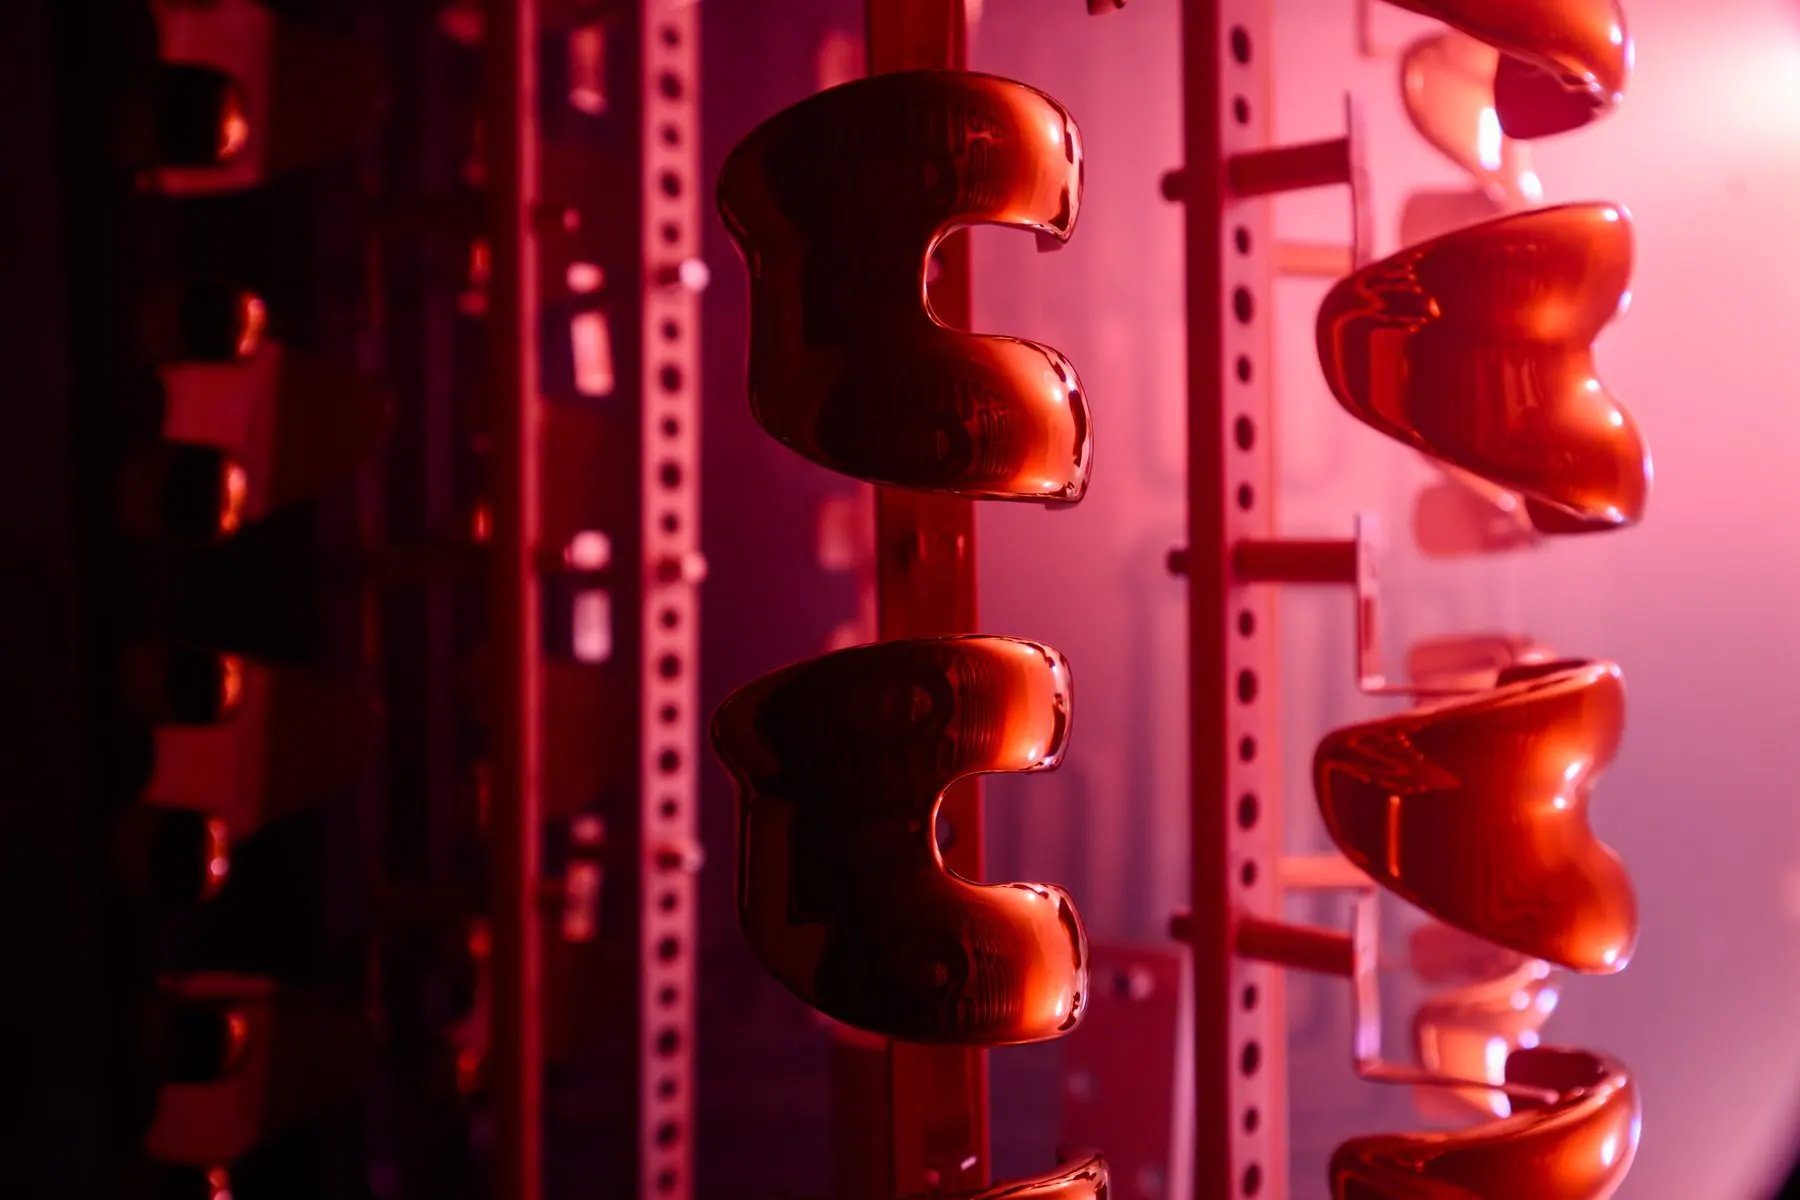
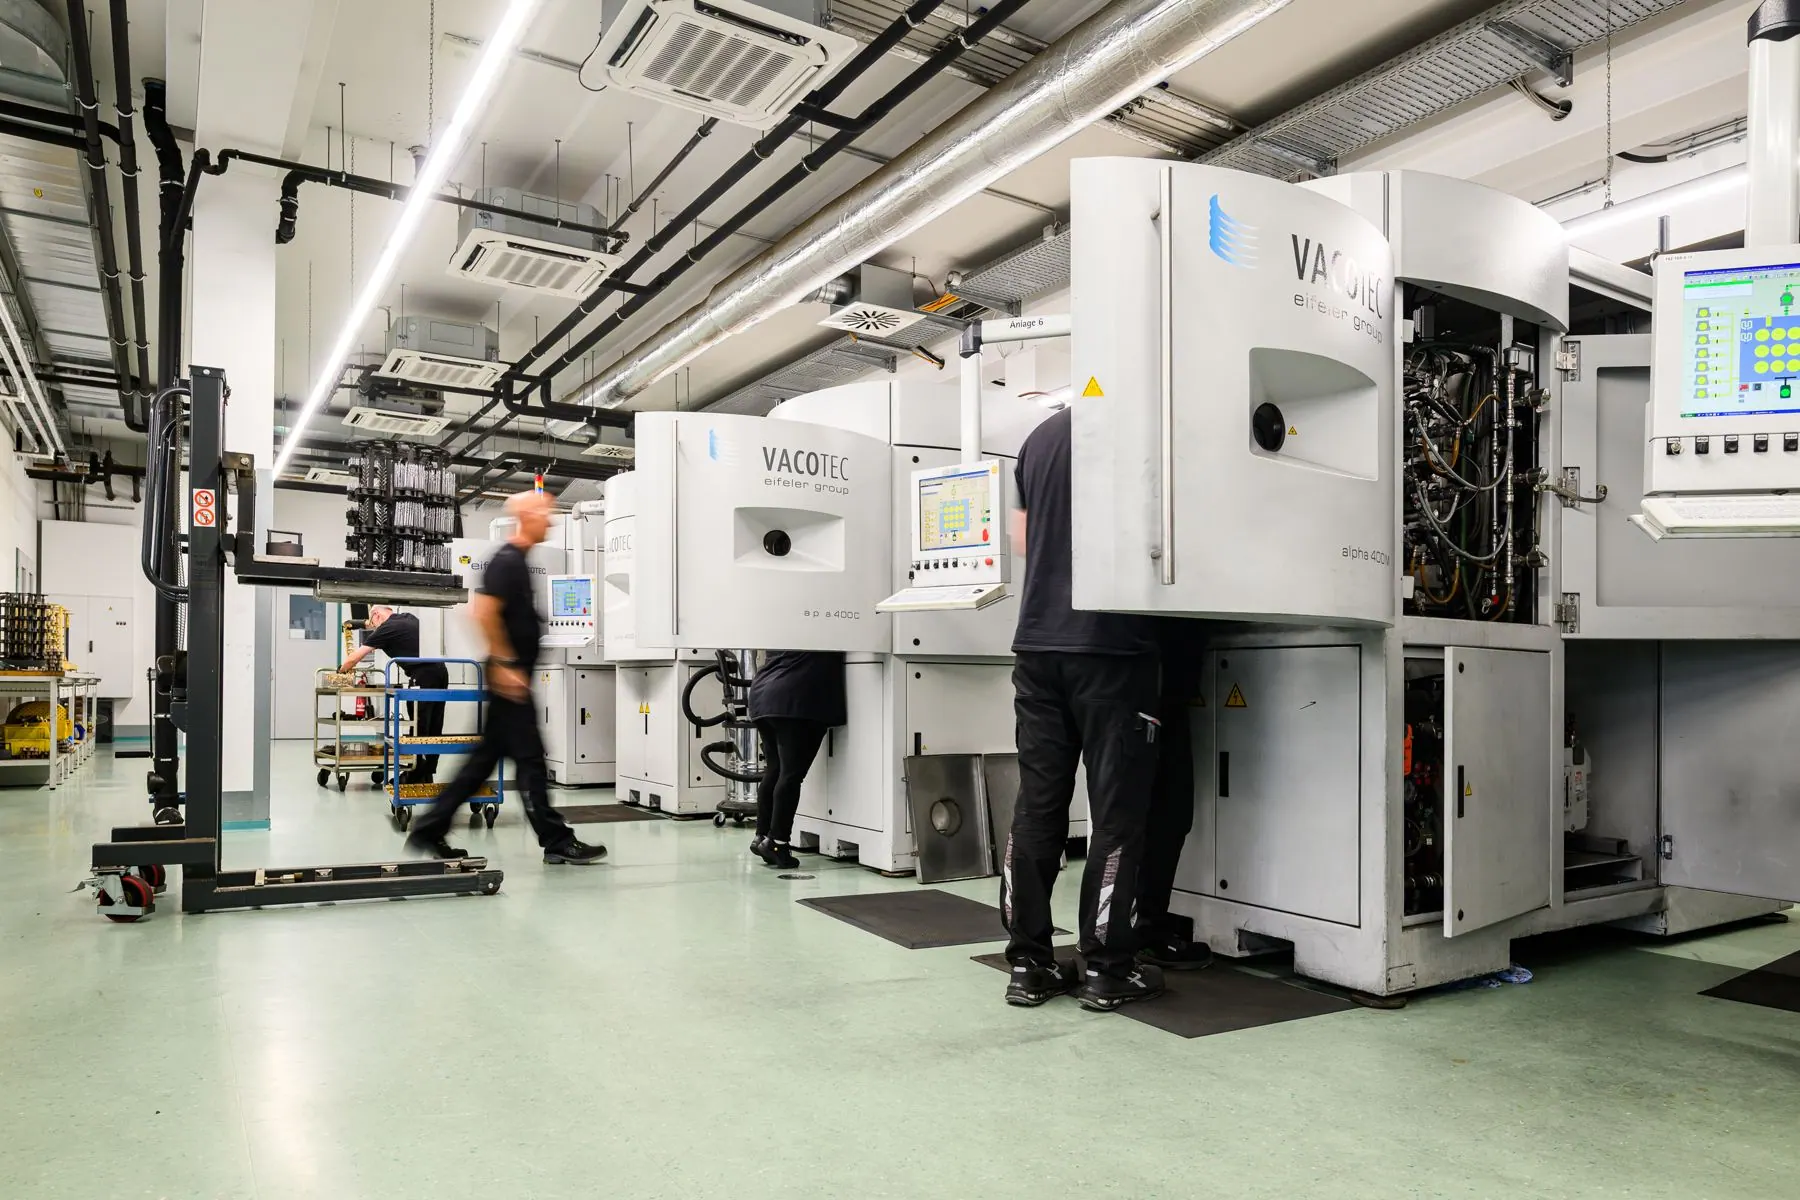
An arc in a vacuum. Ceramic on metal.
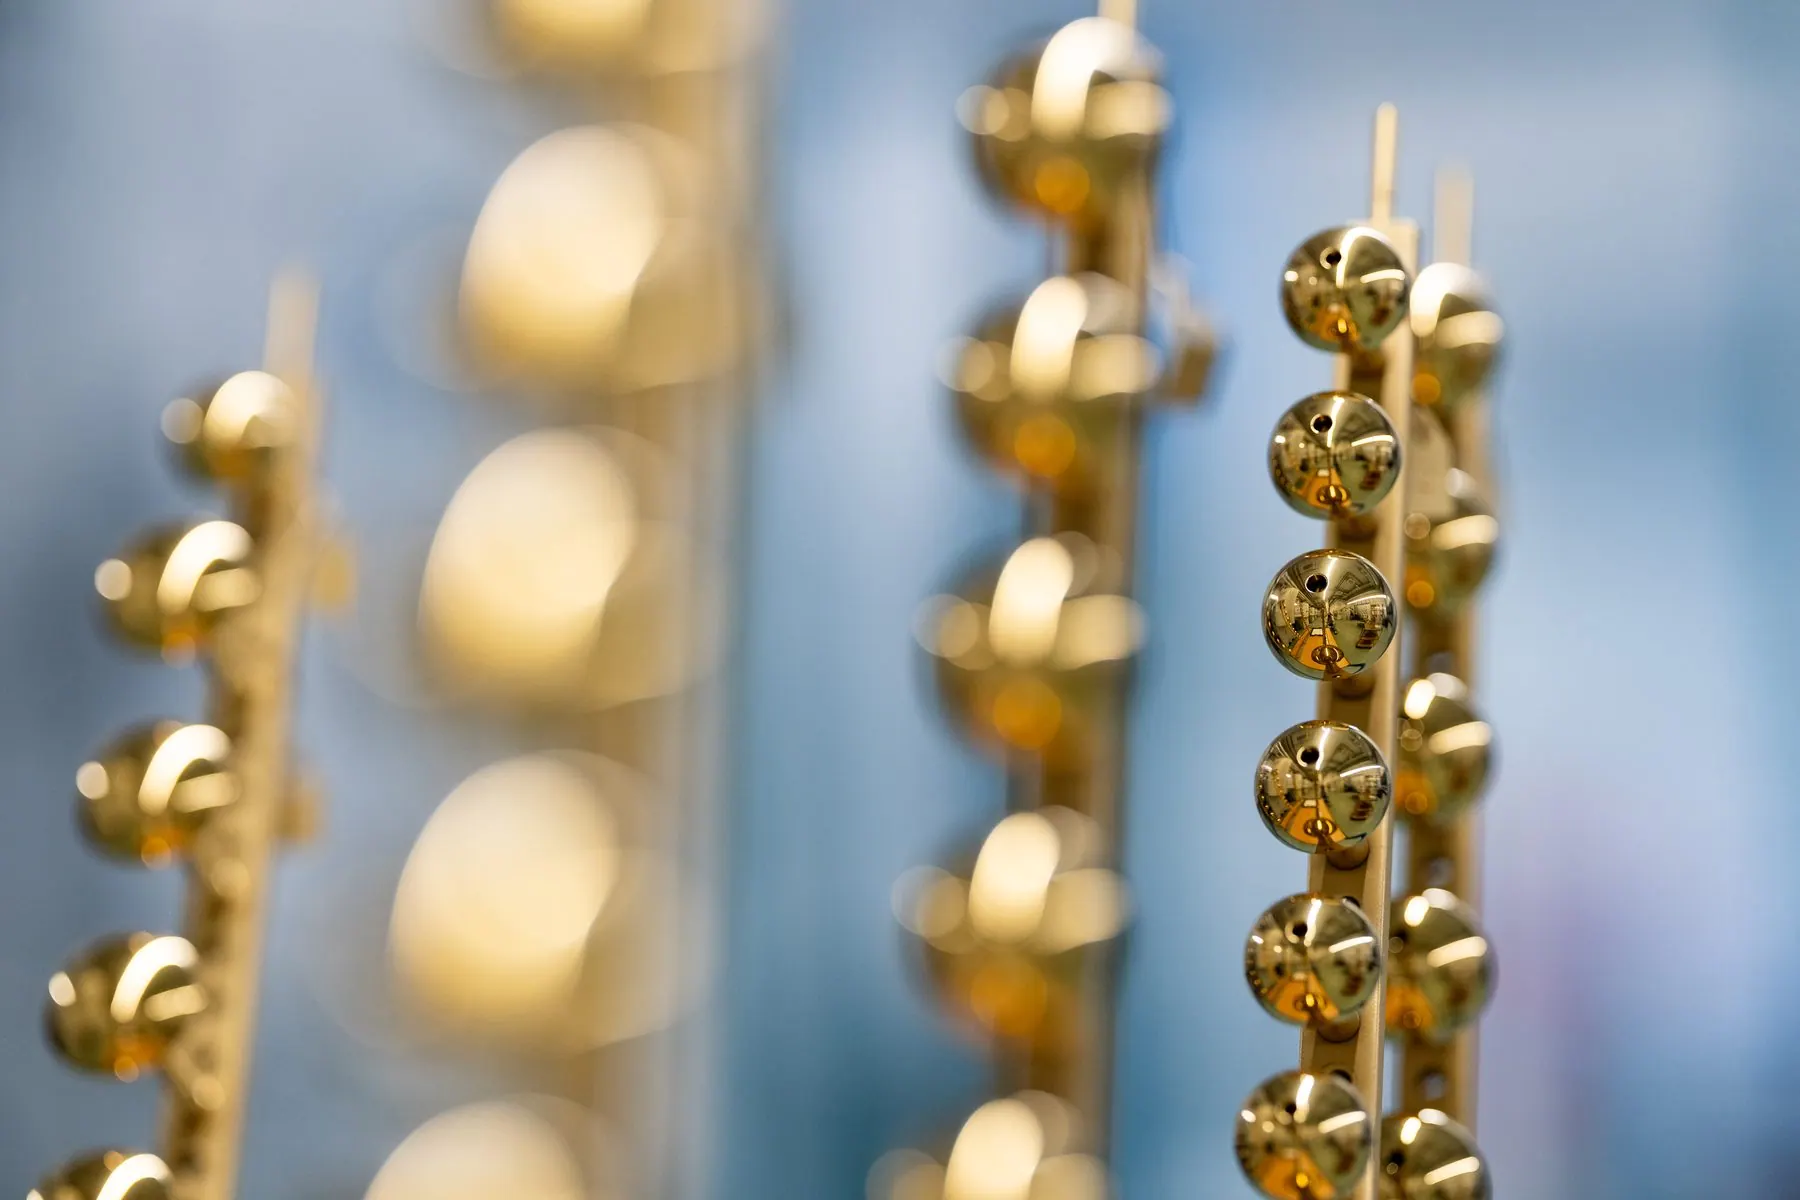
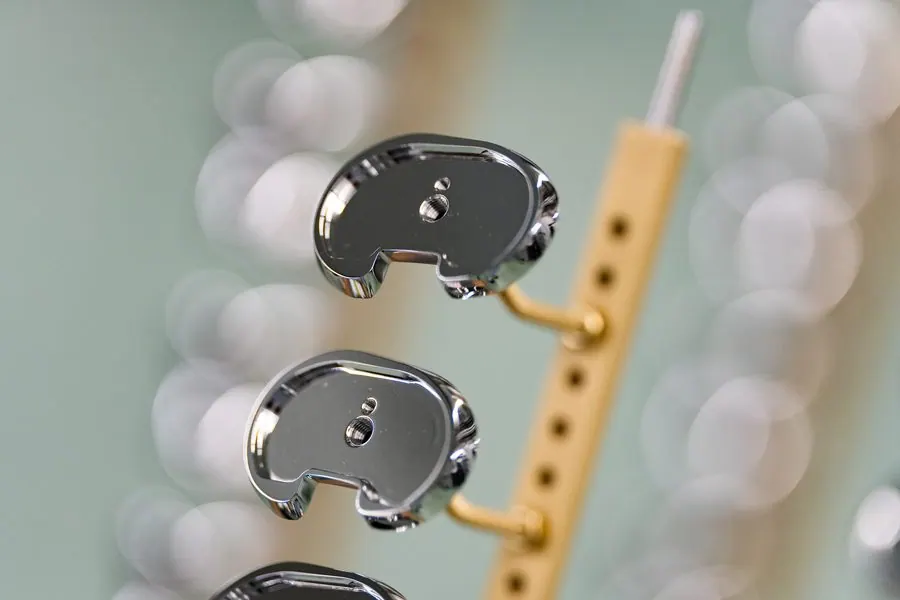
The coatings are produced by arc evaporation (arc PVD) with nitrogen added. They reduce wear on the bearing surface and ion release from the base material. The colour also identifies the coating: TiN gold, ZrN champagne, DLC anthracite.
Five coatings, one plant technology.
The choice depends on the task: bearing couple, cutting edge or appearance. DLC is a metal-containing, amorphous carbon coating of chromium and carbon with a low coefficient of friction.
| Coating | Thickness | Hardness | Adhesion | Use |
|---|---|---|---|---|
| TiN | 0.5 – 7 µm | ~2,300 HV | HF ≥ 1 | Joints, instruments, dental |
| TiNbN | 0.5 – 6 µm | ~2,500 HV | HF ≥ 1 | Knee, bearing couples |
| TiAlN | 0.5 – 6 µm | ~2,700 HV | HF ≥ 1 | Heavily loaded instruments |
| ZrN | 0.5 – 6 µm | ~2,500 HV | HF ≥ 1 | Joints, dental |
| DLC | 0.5 – 2.5 µm | ~700 HV | HF 1 – 3 · DIN 4856 | Rotating and cutting instruments |
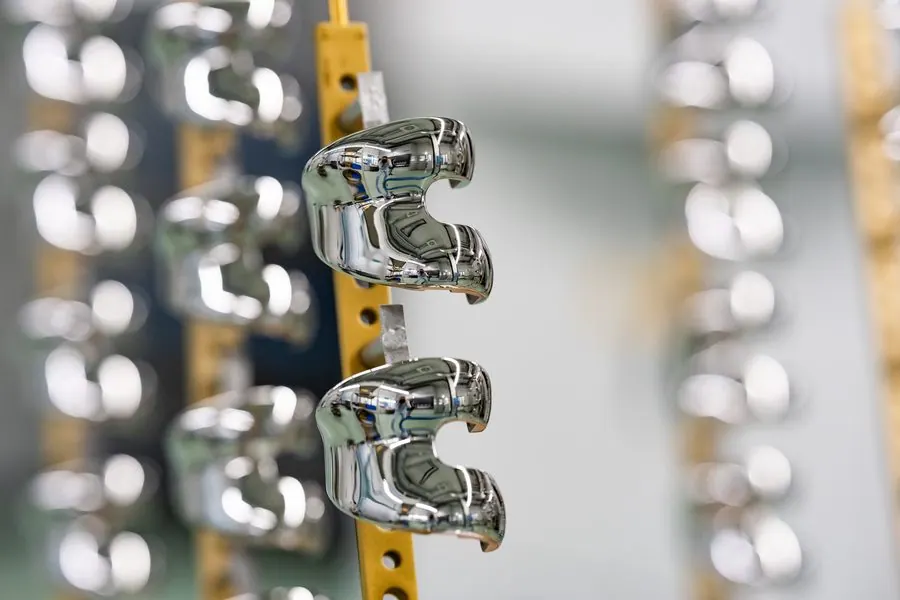
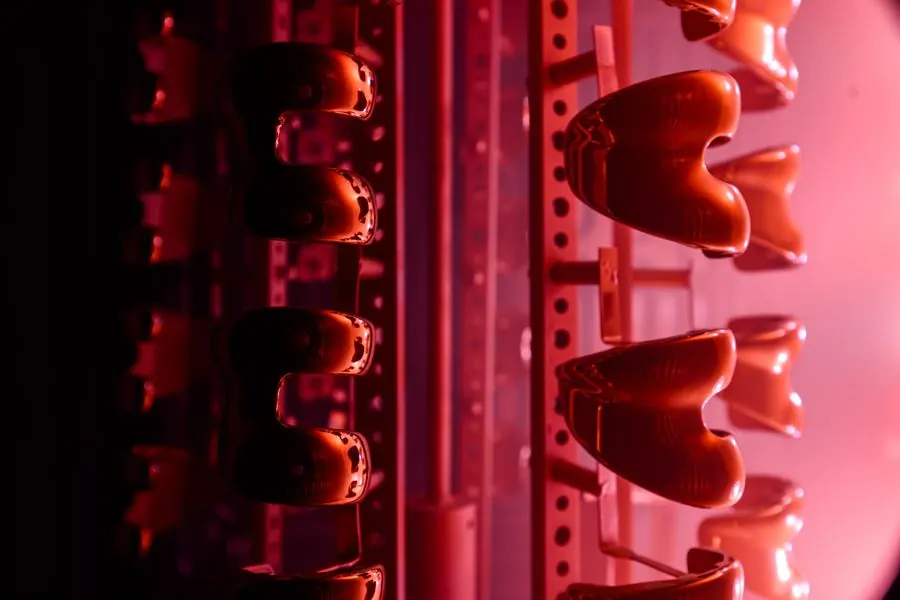
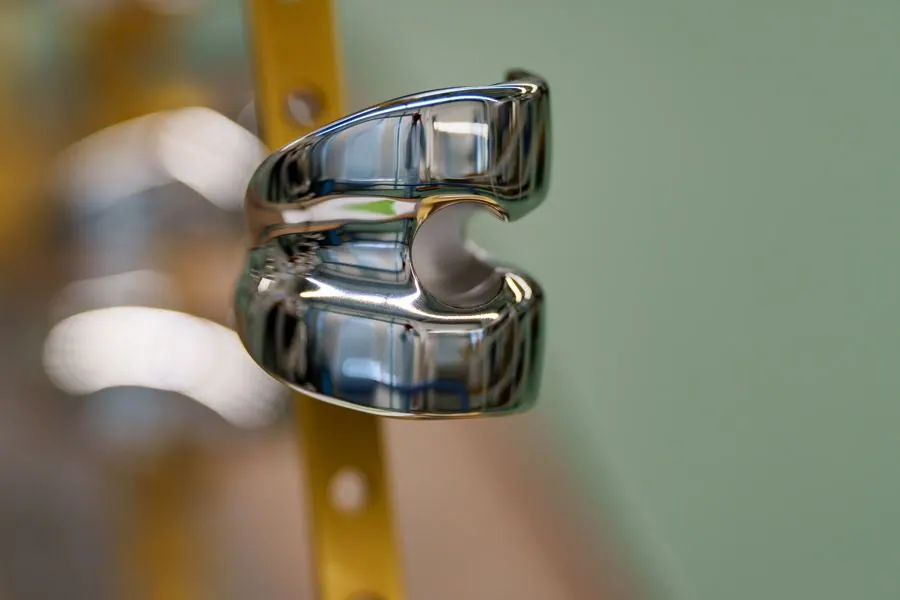
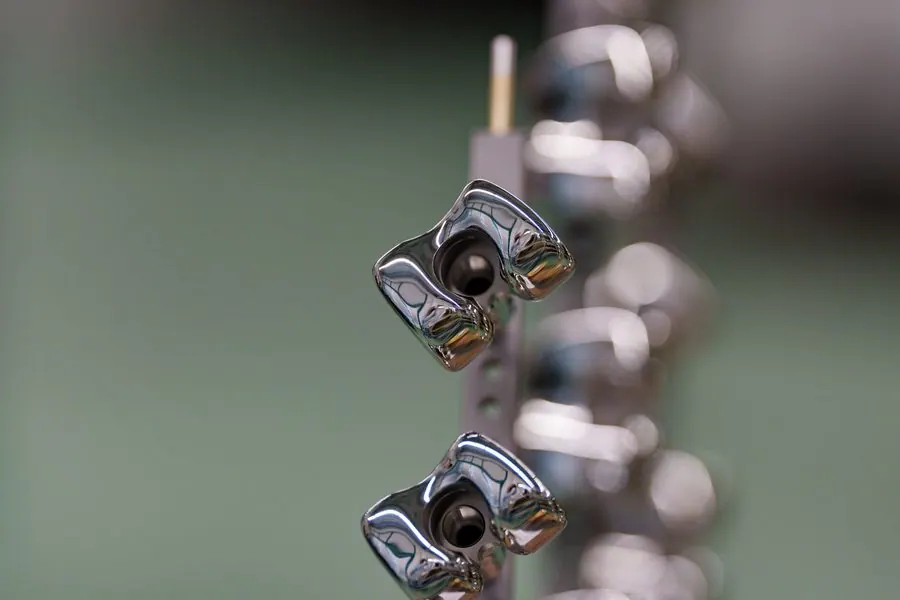
Which coating for what.
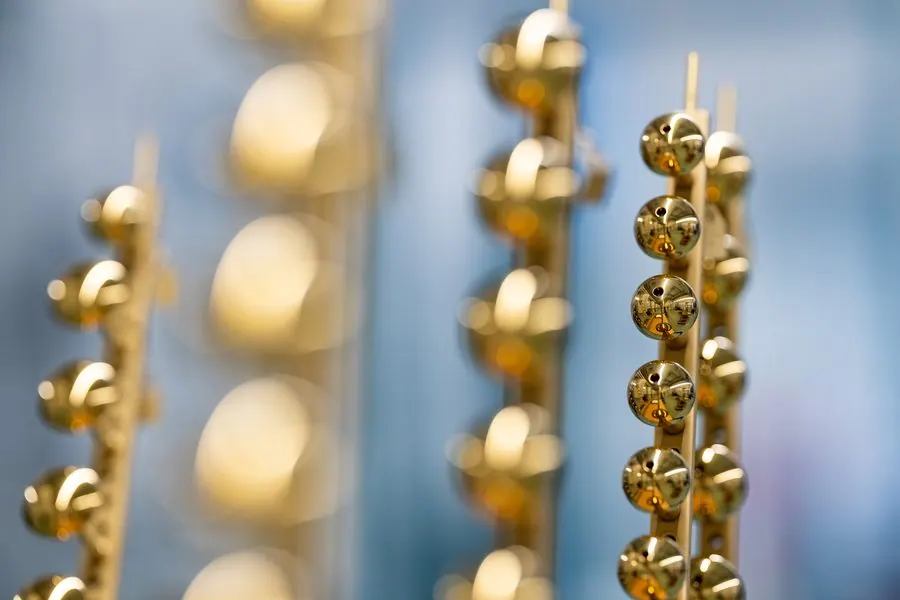
Titanium nitride
Gold colour, high hardness, chemically stable over the long term. For joint components, instruments and dental components.
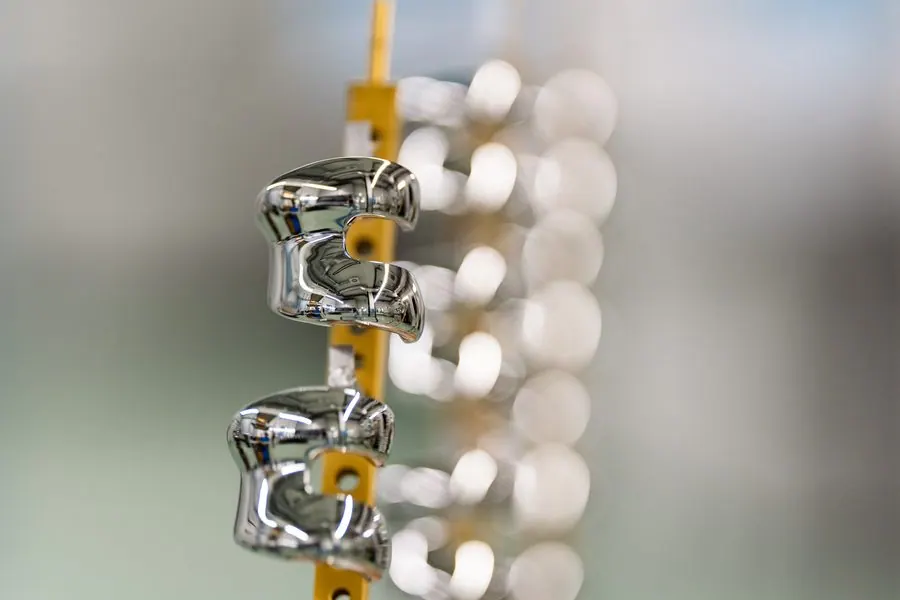
Titanium niobium nitride
The standard choice for bearing surfaces on knee and hip components: harder than TiN, reduced wear, lower allergy potential.
Titanium aluminium nitride
The hardest variant in the range. For heavily loaded instruments and tools.
Zirconium nitride
Nickel-free alternative with a light, golden-yellow colour. For joint components as well as dental components and instruments.
Diamond-like carbon
Amorphous carbon coating with a very low coefficient of friction. Extends the service life of rotating and cutting instruments, including in dental technology.
Titanium, steel, cobalt-chromium, cemented carbide.
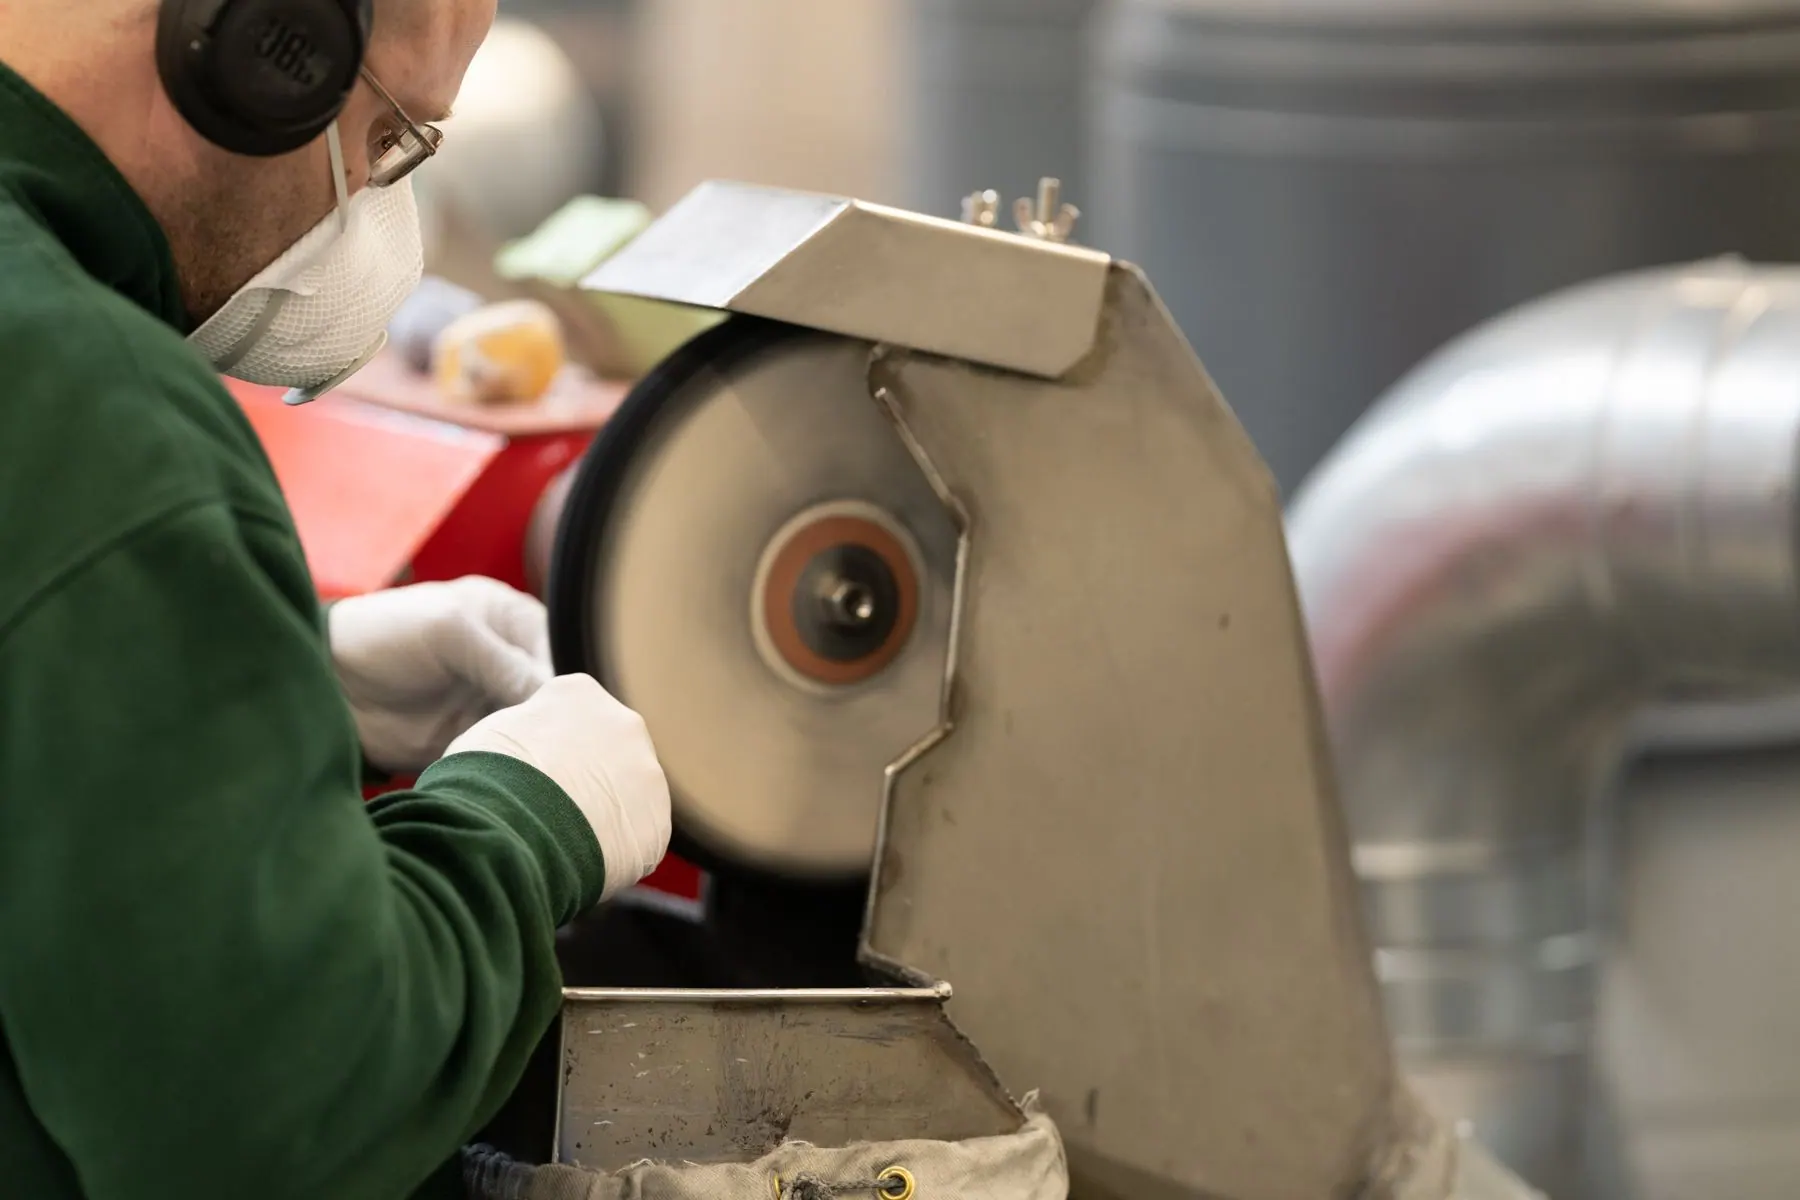
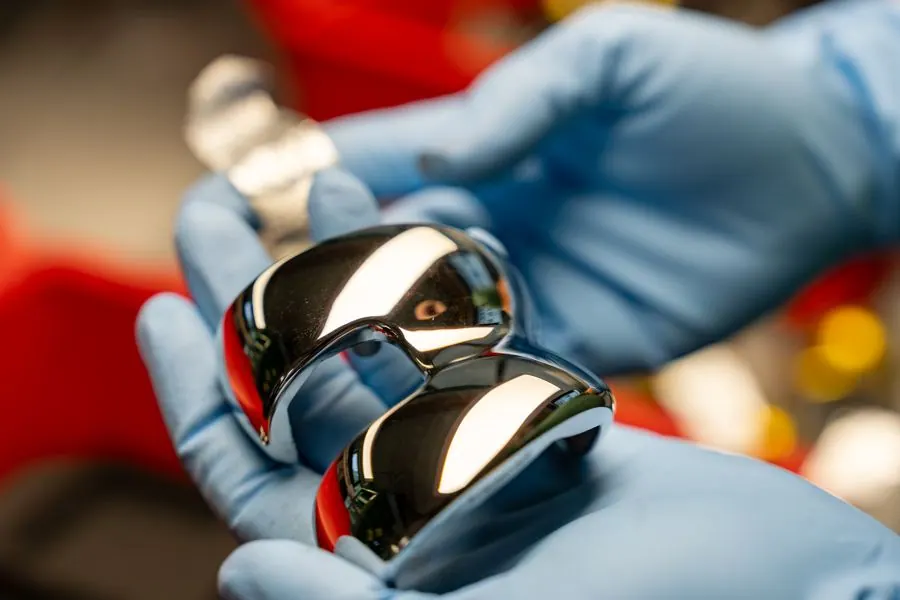
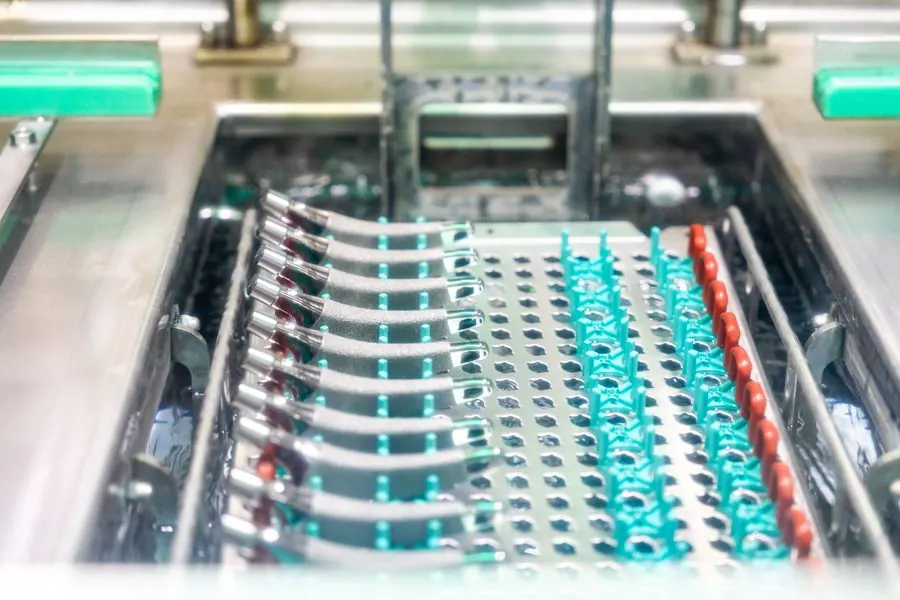
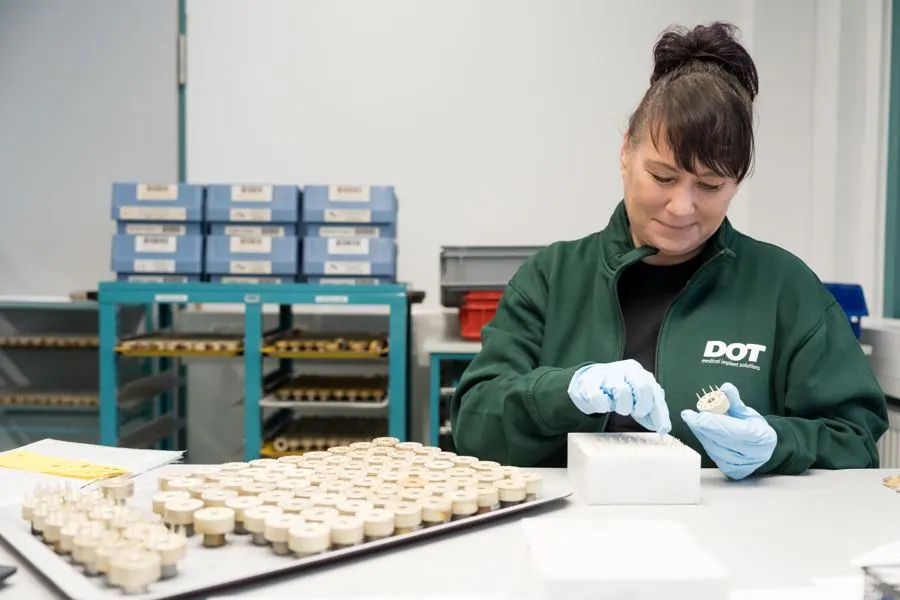
Surface preparation by technical polishing and cleaning is done in house, because the quality of the coating depends on the initial condition.
- Knee: femoral and tibial components with TiNbN or ZrN
- Hip and shoulder: heads and bearing partners
- Instruments: surgical and rotating instruments, DLC since 2012 also for dental tools
- Dental: abutments and instruments with TiN, ZrN or DLC
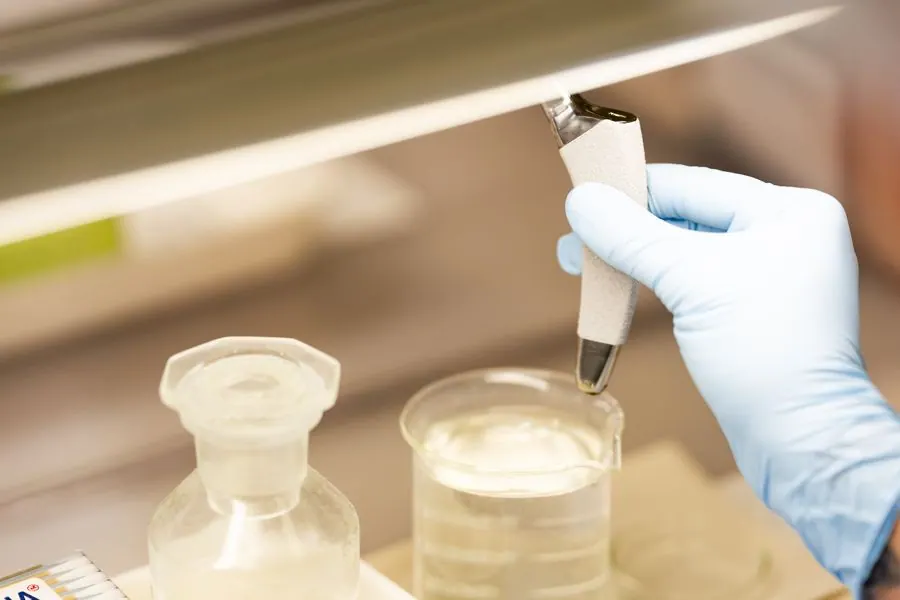
Every batch goes through our own laboratory.
Production has been running since November 2019 in Building 4, built specifically for it, and is part of the quality management system certified to ISO 13485. The results are sent to the customer with the test report.
Polishing and cleaning Rostock
Technical polishing, washing, visual inspection.
Coating Arc PVD
Arc evaporation in a vacuum, nitrogen as reactive gas.
Testing Test laboratory
Coating thickness in cross-section, adhesion by Rockwell indentation test, microhardness, roughness.
Release
Visual and dimensional inspection, test report per batch.
Questions from purchasing and development.
Which base materials can be PVD-coated?
Does the PVD coating change the dimensions of the part?
How is adhesion verified?
Is the coating suitable for patients with metal allergies?
Can DOT also handle polishing before coating?
Bearing surface, instrument or tool: send us the drawing.
You will receive a recommendation on the coating variant, target thickness and scope of testing.